MFR Test Condition: FA/FB series(270℃, 10kg); FC series(310℃, 10kg)
Specificationofbondedneodymiummagneticcompounds
Grade
Br
ResidualFluxDensity
HcB
CoerciveForce
HcJ
IntrinsicCoerciveForce
(BH)max
MaximumEnergyProduct
Molddensity
MeltFlowRate
IZOD
ImpactStrength
TensileStrength
FlexuralStrength
Composition
mT
Gs
kA/m
Oe
kA/m
Oe
kJ/m3
MGOe
g/cm3
g/10min
kJ/m2
MPa
MPa
NdFeB+PA12
NB30
403
4030
242
3040
406
5100
24.9
3.13
4.87
490
19
67
120
NB30L1
386
3860
261
3280
654
8210
25.3
3.18
4.26
1200
15
61
107
NB40
454
4540
301
3780
669
8400
34.2
4.30
4.51
790
17
62
111
NB50
501
5010
315
3960
641
8050
40.0
5.02
4.90
610
18
66
118
NB60
562
5620
354
4450
684
8590
51.0
6.41
5.11
420
16
67
121
NB70
602
6020
368
4620
663
8330
57.2
7.19
5.34
1010
8
54
91
NB80
640
6400
379
4760
632
7940
63.8
8.02
5.64
680
9
62
105
NC35
414
4140
276
3470
592
7430
28.6
3.59
4.57
880
7
55
104
NdFeB+PPS
NC40H-PN
450
4500
320
4020
930
11680
35.4
4.45
4.64
640
10
68
126
NC55A
520
5200
357
4480
917
11520
46.2
5.80
5.05
310
9
61
126
NC60A
532
5320
363
4560
858
10780
48.1
6.04
5.10
320
9
61
127
NC65
574
5740
372
4670
693
8700
53.7
6.74
5.21
110
8
48
108
NC65H2
566
5660
379
4760
826
10370
53.5
6.72
5.29
370
7
57
106
NFB30
408
4080
234
2940
400
5030
26.0
3.27
4.66
400
16
56
114
Ferrite+NdFeB+PA12
NFC30
391
3910
240
3010
457
5740
26.7
3.35
4.42
210
9
56
124
Ferrite+NdFeB+PPS
HNB120a
736
7360
488
6130
973
12220
95.9
12.05
4.75
600
13
50
85
AnisotropicNdFeB+PA12
HNB140a
821
8210
501
6290
1003
12600
113.0
14.20
5.15
400
7
47
83
HNC80a
620
6200
407
5110
971
12200
66.1
8.3
4.35
500
12
47
100
AnistropicNdFeB+PPS
HNC90a
643
6430
421
5290
963
12100
72.4
9.1
4.50
300
10
45
95
HNC100a
670
6700
454
5700
947
11900
80.4
10.1
4.70
200
9
44
95
MFR Test Condition:NB/NFB/HNB series (270C, 10kg); NC/NFC/HNC series(310℃, 10kg).
Specification of Sm-Fe-N series bonded magnetic compounds
Grade
Br
ResidualFluxDensity
HcB
CoerciveForce
HcJ
IntrinsicCoerciveForce
(BH)max
MaximumEnergyProduct
Mold density
Melt Flow Rate
IZOD
ImpactStrength
Tensile Strength
Flexural Strength
Composition
mT
Gs
kA/m
Oe
kA/m
Oe
kJ/m3
MGOe
g/cm3
g/10min
kJ/m2
MPa
MPa
HSFD30b
373
3730
204
2560
384
4820
26.3
3.30
3.80
70
15
47
80
Ferrite+SmFeN+PA11/PA12
HSFD40b
440
4400
243
3050
500
6280
34.2
4.30
3.90
70
14
47
77
HSFD50b
490
4900
282
3540
521
6550
41.8
5.25
4.00
80
14
45
78
HSFD60b
539
5390
321
4030
541
6800
50.7
6.37
4.05
80
14
45
79
HSFD70b
569
5690
349
4380
551
6920
58.1
7.30
4.10
80
14
44
75
HSD80b
603
6030
403
5060
621
7800
66.8
8.39
4.15
70
18
47
79
SmFeN+PA11/PA12
HSD90b
639
6390
406
5100
613
7700
72.8
9.15
4.27
60
15
45
77
HSD100b
653
6530
407
5110
589
7400
78.1
9.81
4.35
60
13
44
79
HSD110b
685
6850
426
5350
569
7150
86.4
10.85
4.53
60
13
41
71
HSND100a
689
6890
408
5130
701
8810
82.0
10.30
4.45
150
13
47
99
AnisotropicNdFeB+SmFeN+PA11/PA12
HSND120a
781
7810
454
5700
812
10200
99.3
12.47
4.95
100
12
50
91
HSND140a
820
8200
496
6230
876
11000
110.6
13.90
5.15
300
10
52
86
HSND150a
840
8400
501
6290
836
10500
118.2
14.85
5.28
230
9
50
83
MFR Test Condition: HSFD/HSD series(240°C,10kg); HSND series(270°C,10kg);
Injection Molded Technology by Chase
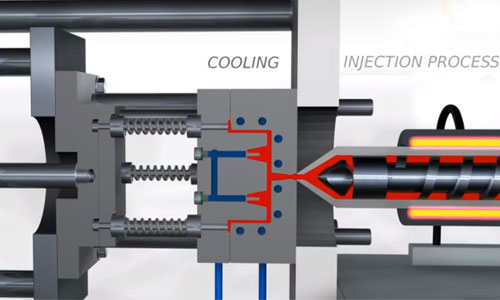
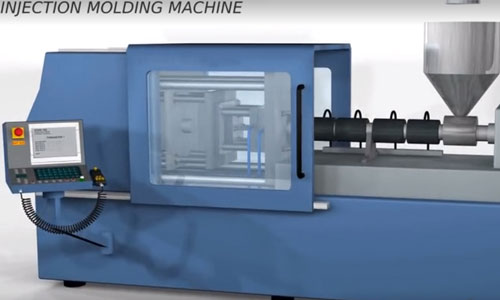
We support customers by optimizing processing parameters based on specific material characteristics to achieve the best balance of magnetic and mechanical performance in plastic bonded magnets. Through close technical collaboration, we work with customers to analyze manufacturing challenges and continuously improve process stability and product consistency.
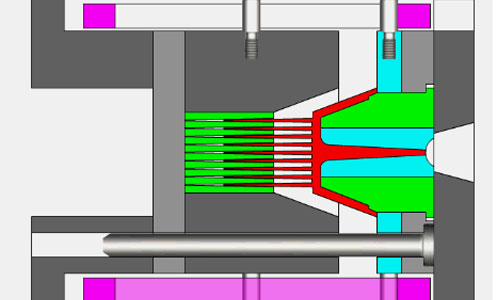
Different plastic bonded magnet systems, especially those based on neodymium magnets, place distinct demands on both material formulation and mold design. Due to the high loading of magnetic powder within the polymer matrix, bonded magnetic composites exhibit significantly lower flowability than conventional plastic compounds. As the magnetic powder content increases, material toughness decreases, increasing the risk of common injection molding defects such as incomplete cavity filling, part cracking, and unstable magnetic properties.
To address these issues, we provide application-specific material and design solutions, including improving melt flow and toughness, reducing friction between the melt and the mold surface, and minimizing internal stress within the molded parts. With extensive project experience and a comprehensive technical solution portfolio in injection-molded magnetic compounds, Chase Technology enables customers to overcome production and design challenges associated with plastic bonded neodymium magnets, ensuring reliable performance and manufacturability at scale.