

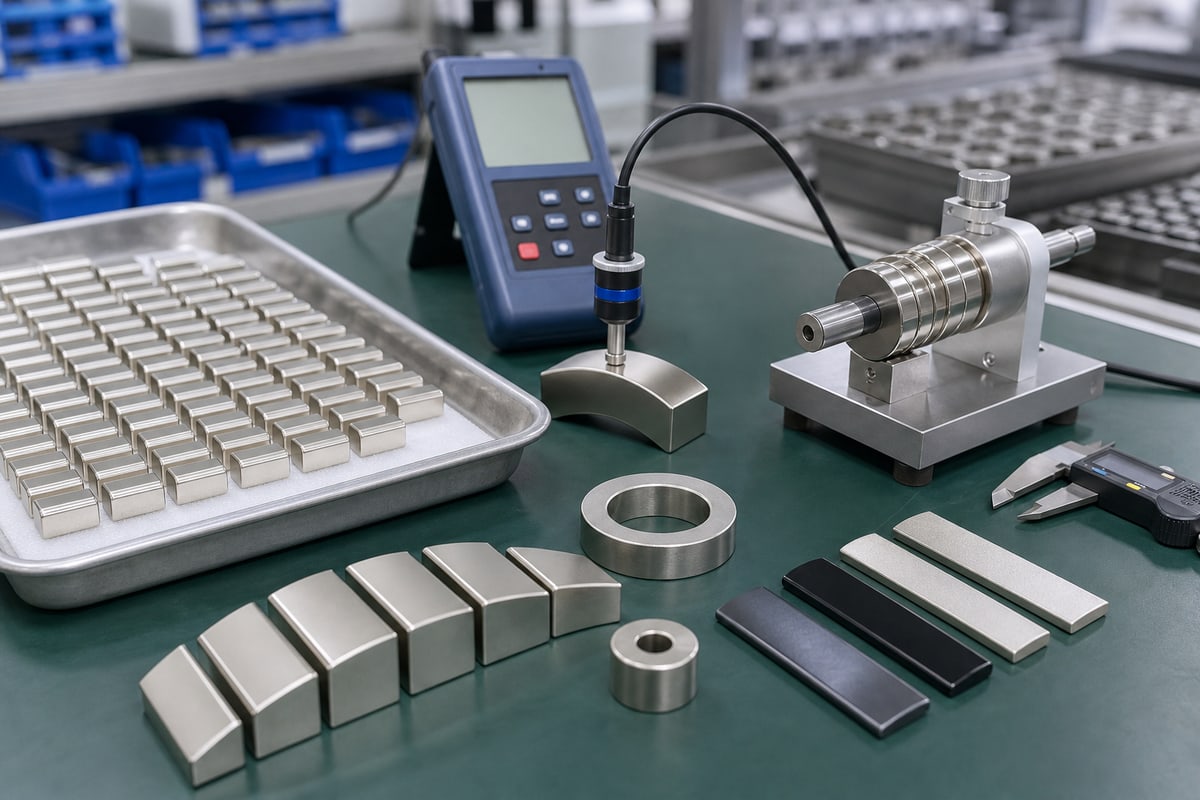
Evaluating a supplier for custom automobile magnets requires more than checking price, ISO certificates, or a sample that meets one gauss reading. Automotive programs need controlled material, geometry, magnetization, validation, traceability, and change management from prototype through serial production. A capable supplier should show how its process repeatedly meets the drawing and application requirements, not simply promise that it can make the part.
This guide gives engineering, quality, and sourcing teams a practical way to qualify magnet suppliers for sensors, electric pumps, actuators, small motors, thermal-management devices, and other vehicle systems.
Evaluating Custom Automobile Magnet Suppliers
Start with application risk, then score the supplier across automotive quality systems, magnet engineering, test capability, production control, and commercial resilience. Require objective evidence at each stage: certificates, process flows, measurement studies, capability data, sample reports, traceability records, and an agreed PPAP plan.
Define the Application Before the RFQ
A useful request for quotation states more than dimensions and magnet grade. Give the supplier the operating temperature range, target field or waveform, sensing air gap, pole count, magnetization direction, corrosion exposure, mechanical loads, mating materials, annual volume, service life, and restricted-substance requirements. Identify any special characteristics on the drawing.
Incomplete requirements force suppliers to make assumptions and make quotations difficult to compare.
Use a Weighted Supplier Scorecard
| Evaluation area | Suggested weight | Evidence to request |
|---|---|---|
| Automotive quality system | 25% | IATF status, audit results, APQP and PPAP examples |
| Magnet engineering | 25% | Material selection, simulation, DFM, magnetization design |
| Testing and validation | 20% | Measurement methods, MSA, durability reports, calibration |
| Production readiness | 20% | Control plan, capacity, traceability, tooling and change control |
| Commercial resilience | 10% | Lead time, sub-tier controls, contingency and cost breakdown |
Adjust the weights to part risk: emphasize traceability and field consistency for sensor targets, or balance and durability for pump rotors.
1. Verify Automotive Quality Credentials
Check IATF 16949 Scope and Status
Ask for the certificate, site name, scope, expiration date, and issuing certification body. Confirm that the facility making the magnets is covered; a group certificate or a sales-office certificate may not include the production site. The International Automotive Task Force developed common quality-system requirements for automotive production-material and service-part suppliers. Certification is valuable evidence, but it does not replace a product- and process-specific audit.
Review the supplier’s ability to use APQP, Control Plan, PPAP, FMEA, MSA, and SPC. AIAG identifies these Core Tools as the building blocks of an automotive quality management system. Ask who owns each deliverable and how customer-specific requirements are built into the project plan.
Audit Traceability and Change Control
A traceability exercise should connect a finished lot to magnetic powder or alloy, binder, coating chemicals, molding or sintering batch, machining, magnetizing fixture, inspection results, operator, and shipment. Test how quickly the supplier can isolate affected material. Also require written approval before changes to material source, formulation, tooling, process location, subcontractor, inspection method, or packaging.
2. Assess Custom Magnet Engineering Capability
Compare Materials Against Real Conditions
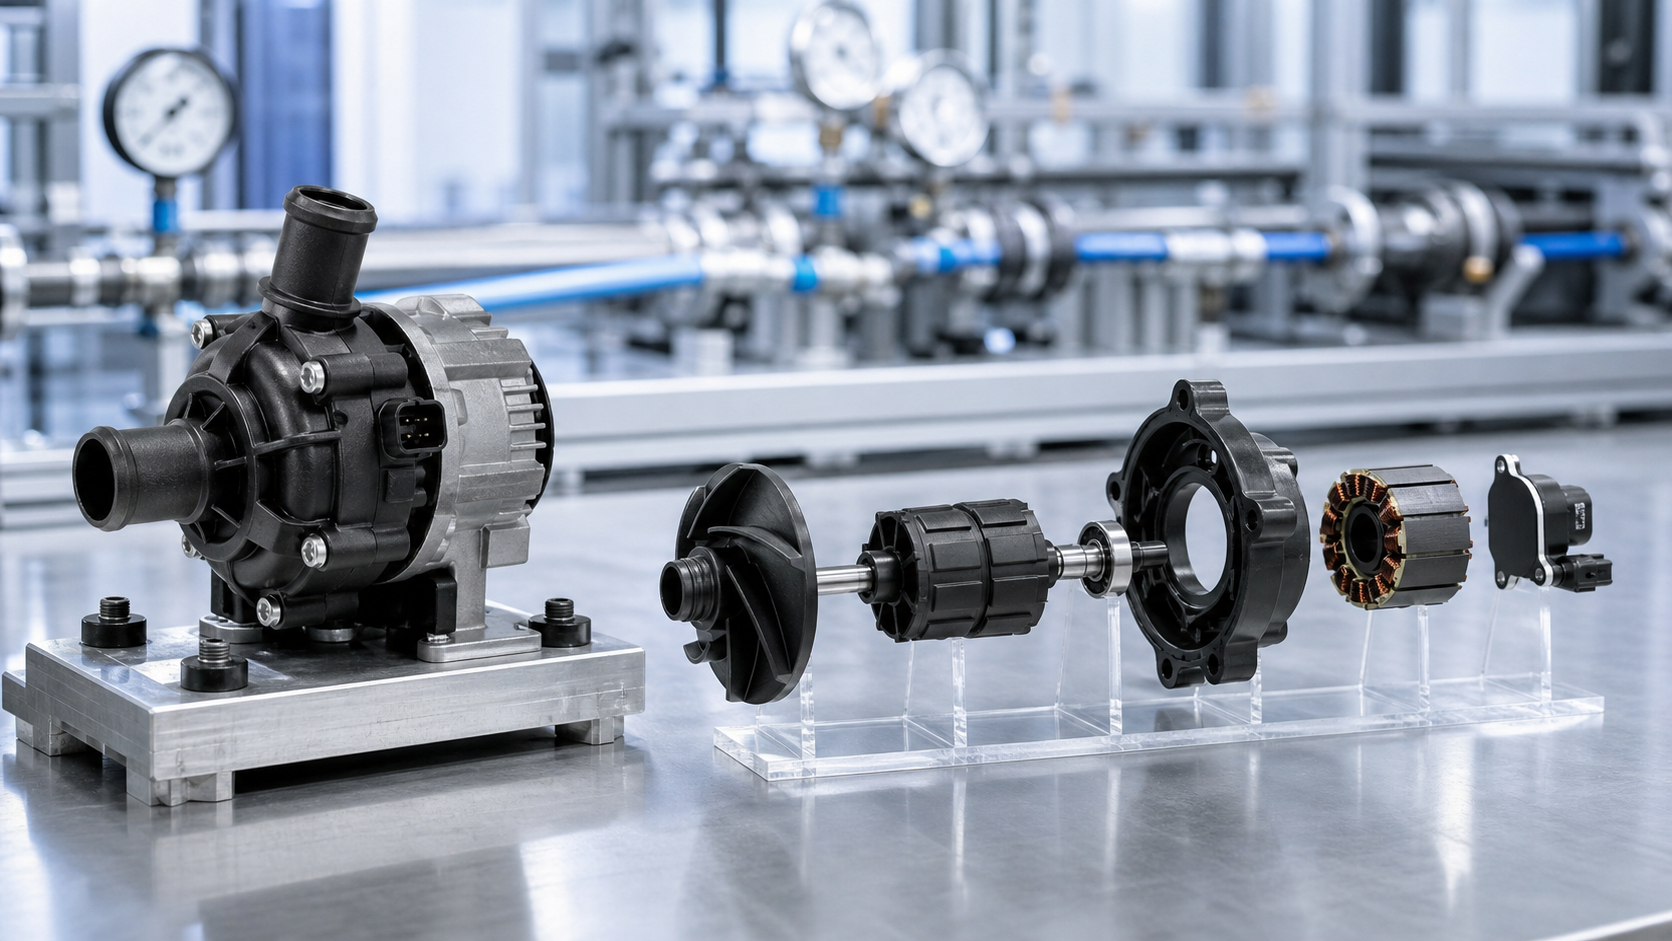
A strong supplier explains why sintered NdFeB, bonded NdFeB, ferrite, SmCo, or SmFeN fits the application. Compare field strength, irreversible temperature loss, corrosion, geometry, integration, and cost. Injection-molded compounds can support complex shapes, multipole magnetization, and inserts, while sintered NdFeB provides higher output where assembly and corrosion controls are acceptable.
Ask the engineering team to document the tradeoff instead of defaulting to the highest grade. Chase Technology’s injection-molded magnet data compares magnetic and mechanical properties across grades.
Review DFM and Magnetization Design
Request a design-for-manufacture review covering tolerances, datum strategy, draft, wall thickness, coating allowance, inserts, adhesive gaps, rotor retention, and poka-yoke features. For sensor rings and rotors, define pole count, pole pitch, indexing, waveform limits, and the measurement path. A supplier with magnetic simulation and in-house magnetizing-fixture capability can identify weak field regions or fixture constraints before tooling is released. See Chase Technology’s magnetic simulation workflow and custom tooling and magnetizing fixtures for the types of evidence an engineering review can produce.
3. Review Magnetic Testing and Validation
Confirm Measurement Methods and MSA
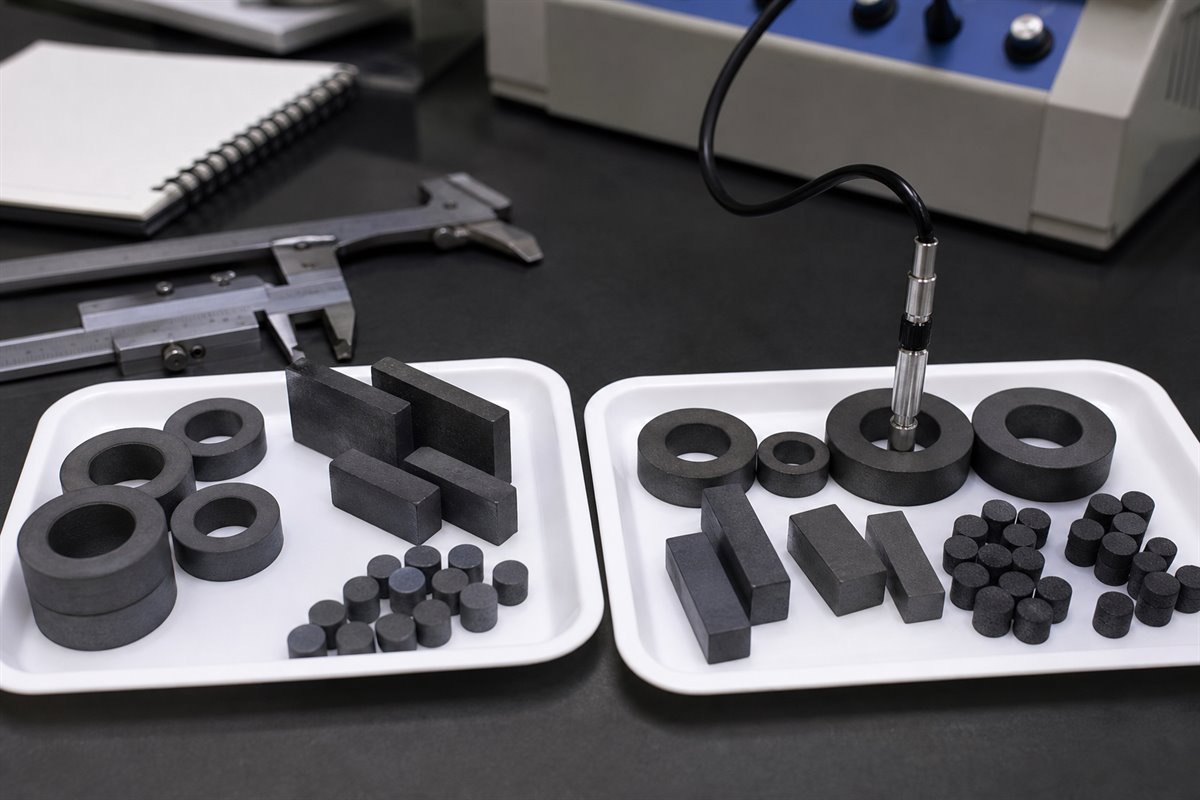
A single surface-gauss value rarely defines an automotive magnet. Agree on the test fixture, probe type, air gap, orientation, temperature, sampling plan, and acceptance limits. Depending on the design, evidence may include hysteresis data, magnetic moment, flux, surface-field mapping, harmonic content, pole-to-pole variation, dimensions, coating thickness, pull force, or rotor balance. Ask for calibration status and gauge repeatability and reproducibility for critical measurements.
Match Durability Tests to the Vehicle
Validation should reproduce the part’s actual environment. Useful tests may include thermal aging, temperature cycling or shock, high-temperature/high-humidity exposure, salt spray, chemical resistance, vibration, mechanical shock, bond strength, and demagnetization margin. Do not accept a standard test menu without checking duration, temperature, fluid, load, and pass criteria against the component specification. Chase Technology lists VSM, three-dimensional field mapping, salt spray, humidity, and thermal-shock resources in its custom magnetic assembly R&D and testing capabilities.
4. Audit Automotive Production Readiness
Examine Process Control and Capacity
Walk through the entire process flow, including any sub-tier operations. Compare the Process FMEA with the control plan and shop-floor instructions. Critical parameters might include powder composition, moisture, molding temperature and pressure, sintering profile, machining, coating bath control, adhesive cure, magnetizing energy, and fixture position. Review capability data from production-intent equipment rather than a laboratory-only sample run.
Capacity evidence should cover cycle time, cavities, uptime, scrap, bottlenecks, maintenance, backup equipment, and surge response. For imports, include packaging, corrosion protection, lead time, and safety stock.
Check Tooling Ownership and Continuity
State who owns molds, dies, gauges, magnetizing fixtures, and inspection fixtures. Record preventive-maintenance intervals, spare inserts, expected tool life, storage location, and replacement rules. Supply continuity also depends on approved sources for rare-earth alloy or magnetic powder, binder, coating, inserts, and outsourced finishing. Ask for a recovery plan for the highest-risk material and process steps.
5. Compare Samples, PPAP, and Total Cost
Use Production-Intent Samples
Prototype samples can confirm direction, but they do not prove serial capability. Ask which material lot, tool, machine, fixture, operator, and inspection method produced each sample. Before approval, agree on PPAP submission level and deliverables such as the design record, process flow, PFMEA, control plan, MSA, dimensional results, material and performance tests, capability studies, appearance approval if relevant, sample parts, and Part Submission Warrant.
Compare Cost on the Same Scope
Normalize quotations for material grade, coating, tolerances, magnetization, testing, packaging, tooling, PPAP, freight, duties, and annual-volume assumptions. A lower piece price can be erased by extra inspection, unstable yield, premium freight, or line interruption. If you need a broader pre-contract screen, pair this automotive checklist with our guide to choosing a reliable neodymium magnet manufacturer.
Automotive Magnet Supplier Questions
- Which automotive applications and magnet processes run at the proposed factory?
- Which IATF 16949 scope and customer-specific requirements apply?
- Who owns DFM, APQP, PPAP, and magnetic validation?
- How are material lots, magnetizing fixtures, and test results traced?
- Which characteristics receive SPC and capability monitoring?
- What changes require customer notification and requalification?
- What is the contingency plan for critical materials, tooling, and equipment?
Build a Lower-Risk Magnet Sourcing Plan
Send the drawing, operating conditions, magnetic targets, validation standard, forecast, and PPAP expectations with your RFQ. Chase Technology can review material, magnetization, tooling, simulation, testing, and production options for automotive sensor rings, pump rotors, actuators, and other custom magnetic parts. Contact us to discuss your custom specs.
FAQs
What Are Custom Automobile Magnets?
They are permanent magnets or magnetic assemblies designed around a vehicle component’s geometry, field, temperature, durability, integration, and production requirements. Common examples include sensor rings, pump rotors, actuator magnets, and small-motor components.
Is IATF 16949 Mandatory?
It depends on the customer, supply-chain position, and sourcing requirements. Even when certification is not contractually mandatory, buyers should require a defined automotive quality system and risk-based supplier development plan.
What Belongs in a Magnet PPAP?
The exact submission level is customer-defined. Typical evidence includes the drawing, process flow, PFMEA, control plan, MSA, dimensions, material and magnetic test results, capability studies, production samples, and Part Submission Warrant.
How Should Magnet Samples Be Tested?
Use agreed fixtures, air gaps, temperatures, sampling, and limits that match the application. Test magnetic output or waveform together with dimensions, mechanical integrity, coating, environmental durability, and any assembly-level characteristics.
When Should a Supplier Audit Happen?
Audit before final sourcing when part risk, new technology, new tooling, or high volume justifies it. Repeat or target the audit after major changes, recurring quality issues, capacity moves, or weak corrective-action performance.